Free Consultation :
EDITION
2026–2027 · Rev 03
Quality Control Plan · BS EN 124-2:2015
Control characteristics, inspection methods, sampling frequencies and acceptance criteria for every stage of manufacture, from charge make-up to container seal.
Work stops until QX releases it in writing.
A QX engineer is present for the activity.
QX reviews the records within 24 hours.
QX re-checks a sample of what the foundry released.
QX-recommended value, not set by the standard.
COLOUR CODE OF DECISIONS
Result inside the limit. Work continues.
Result unknown or at risk. Stop and wait for QX release.
Result outside the limit. Quarantine and raise an NCR.
THE THREE RULES OF EVIDENCE
Every check has a time-stamped photograph with the lot or heat number in the frame.
Records are attributable, legible, contemporaneous, original and accurate. Never written from memory.
Heat, lot, pallet and container seal numbers link every piece back to its melt.
We do not simply search for a supplier that says:
“Yes, we can manufacture it.”
We evaluate whether the foundry has the actual technical capability to manufacture it repeatedly.
What exactly is required?
What grade, chemistry and mechanical properties are required?
Can the foundry manufacture the geometry consistently?
Can the pattern and core system produce the required casting?
Can the foundry control the melt, treatment and final structure?
Can the required testing be performed and documented?
Can the supplier deliver the required volume consistently?
Can the finished castings be packed, identified and dispatched correctly?
02 / QX DOCUMENT REGISTER
Five document families and one numbering rule connect the master plan to the work instruction, inspection record and client report.
The rulebooks: parameters, frequencies, standards
QCP-01
Quality Control Plan for Ductile Iron Manhole Covers & Gully Tops (BS EN 124-2:2015)
QCP-02
Quality Control Plan for Cast Access Covers & Grates (AS 3996:2019)
QCP-03
Quality Control Plan for Channel Drainage Systems & Gratings (EN 1433)
QCP-04
Generic Quality Control Plan for Ferrous OEM & Machinery Castings
System level: who does what, when and how
SOP-01
Foundry Identification, Capability Assessment & Onboarding Procedure
SOP-02
New Product Development (NPD), Pattern Tooling & DFM Protocol
SOP-03
In-Process Production Monitoring & Shop-Floor WIP Tracking
SOP-04
Finished Goods Pre-Shipment Inspection (PSI) Procedure & AQL Sampling
SOP-05
Proof-Load & Permanent Set Testing Witnessing Procedure (EN 124 / AS 3996)
SOP-06
Non-Conformance Handling, Defect Investigation & CAPA (8D Process)
SOP-07
Anti-Rust Coating, Seaworthy Packaging & Container Loading Supervision
SOP-08
Field Inspector Code of Conduct, Ethics & Anti-Bribery Policy
Step by step, in the inspector’s hand at the foundry
WI-01
Spectrometer Calibration, Spark Test & Melt Chemistry Verification
WI-02
Green Sand Testing & Moulding Parameter Verification
WI-03
Pattern, Core-Box Tooling & Draft Angle Verification
WI-04
Visual Surface Defect Identification & Acceptance Criteria
WI-05
Dimensional & Gauge Mapping (Clear Opening, Flanges & Seating Planarity / Anti-Rock)
WI-06
Microstructure, Nodularity & Brinell Hardness Verification
WI-07
Bitumen / Paint Dry Film Thickness (DFT) Gauge Measurement
WI-08
Container Structural Inspection, Dunnage & Maritime Packing Check
The fillable forms that become the client report
IRF-01
Foundry Technical Capability & Infrastructure Audit Scorecard (100-Point Audit)
IRF-02
New Tooling & First Article Inspection Report (FAIR / PPAP Sheet)
IRF-03
Daily / Weekly Production Monitoring Flash Report
IRF-04
Pre-Shipment Quality Inspection Report (PSI)
IRF-05
BS EN 124 / AS 3996 Proof-Load Test Witness Certificate
IRF-06
Chemical & Mechanical Test Verification Log (Tensile, Hardness, Microstructure)
IRF-07
Non-Conformance Report (NCR) & Corrective Action Form
IRF-08
Container Loading Supervision & Seaworthy Packing Report
Onboarding foreign buyers and protecting QX
DOC-01
Master Services Agreement (MSA) for Quality Governance & Sourcing
DOC-02
Service Level Agreement (SLA) & Rate Card Schedule (A-la-carte, Retainer, Turnkey)
DOC-03
Technical Scope of Work (SOW) Template
DOC-04
Mutual Non-Disclosure Agreement (NDA, International Client)
DOC-05
Bilateral Non-Circumvention & Non-Disclosure Agreement (NCNDA, Local Foundries)
DOC-06
Client Project Onboarding & Technical Requirement Intake Form
So every record can be traced
QCP-nn
master plan
ITP-nn-CCC
order plan from QCP-nn for customer CCC
IRF-nn
form, filed under the visit report
IR-yy-nnn
visit report: year, serial
NCR-yy-nnn
non-conformance: year, serial
SUP-nnn
foundry qualification record
QCP-01 / CONTROLLED QUALITY PLAN
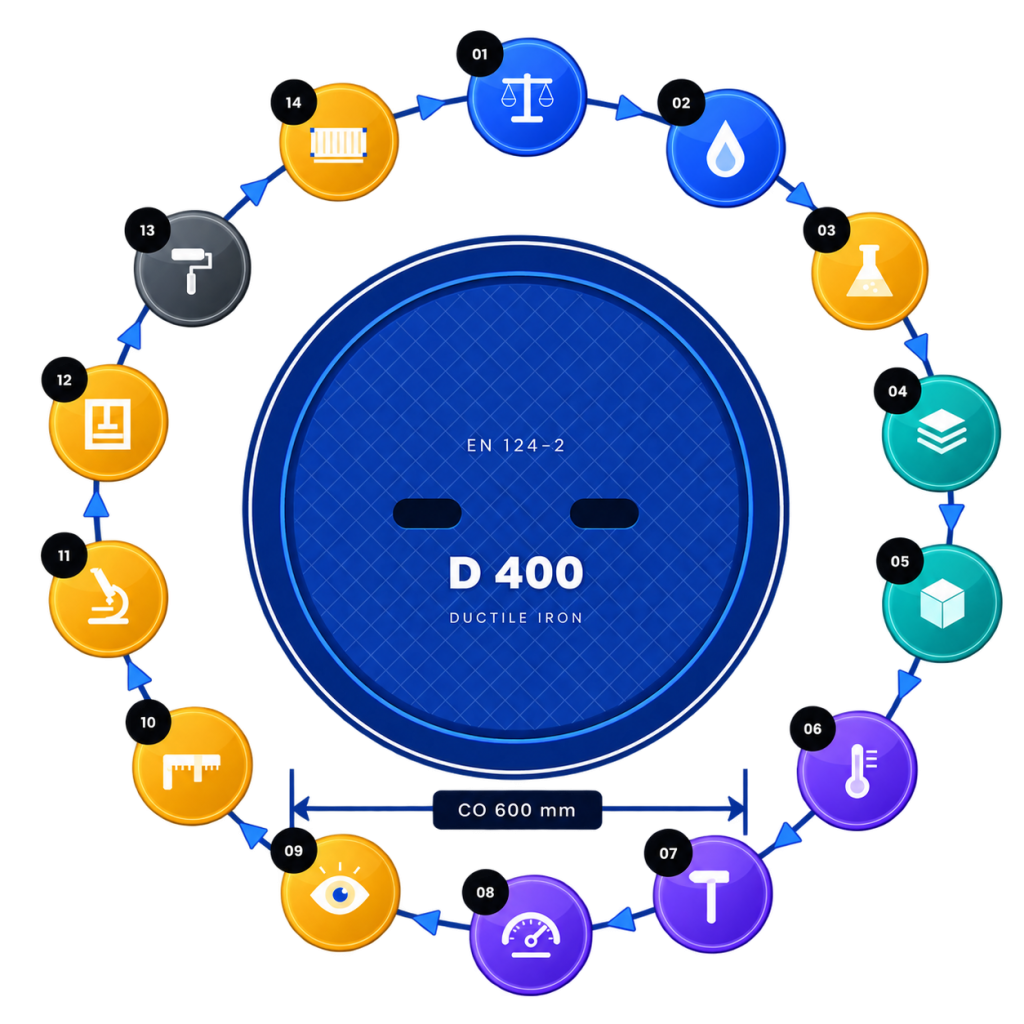
For ductile iron manhole covers and gully tops, QX’s reference plan turns specifications into a staged inspection path. Decisions are backed by photographs, same-day records and traceable heat, lot and dispatch details.
Controlled stages
Control steps
Hold points
Process gates
FIVE LINKED PROCESS GATES
01
Raw material, treatment and chemistry.
02
Sand, tooling and cores.
03
Pouring, cooling and finishing.
04
Fit, properties and performance.
05
Coating, packing and final release.